DE
 EN
 FR

Tiana
+86-13143789995
10 % Punkterückerstattung bei benutzerdefinierten Druckaufträgen. Jetzt aktivieren
Brauchen Sie Hilfe? Sprechen Sie noch heute mit einem Druckexperten. Händlersuche
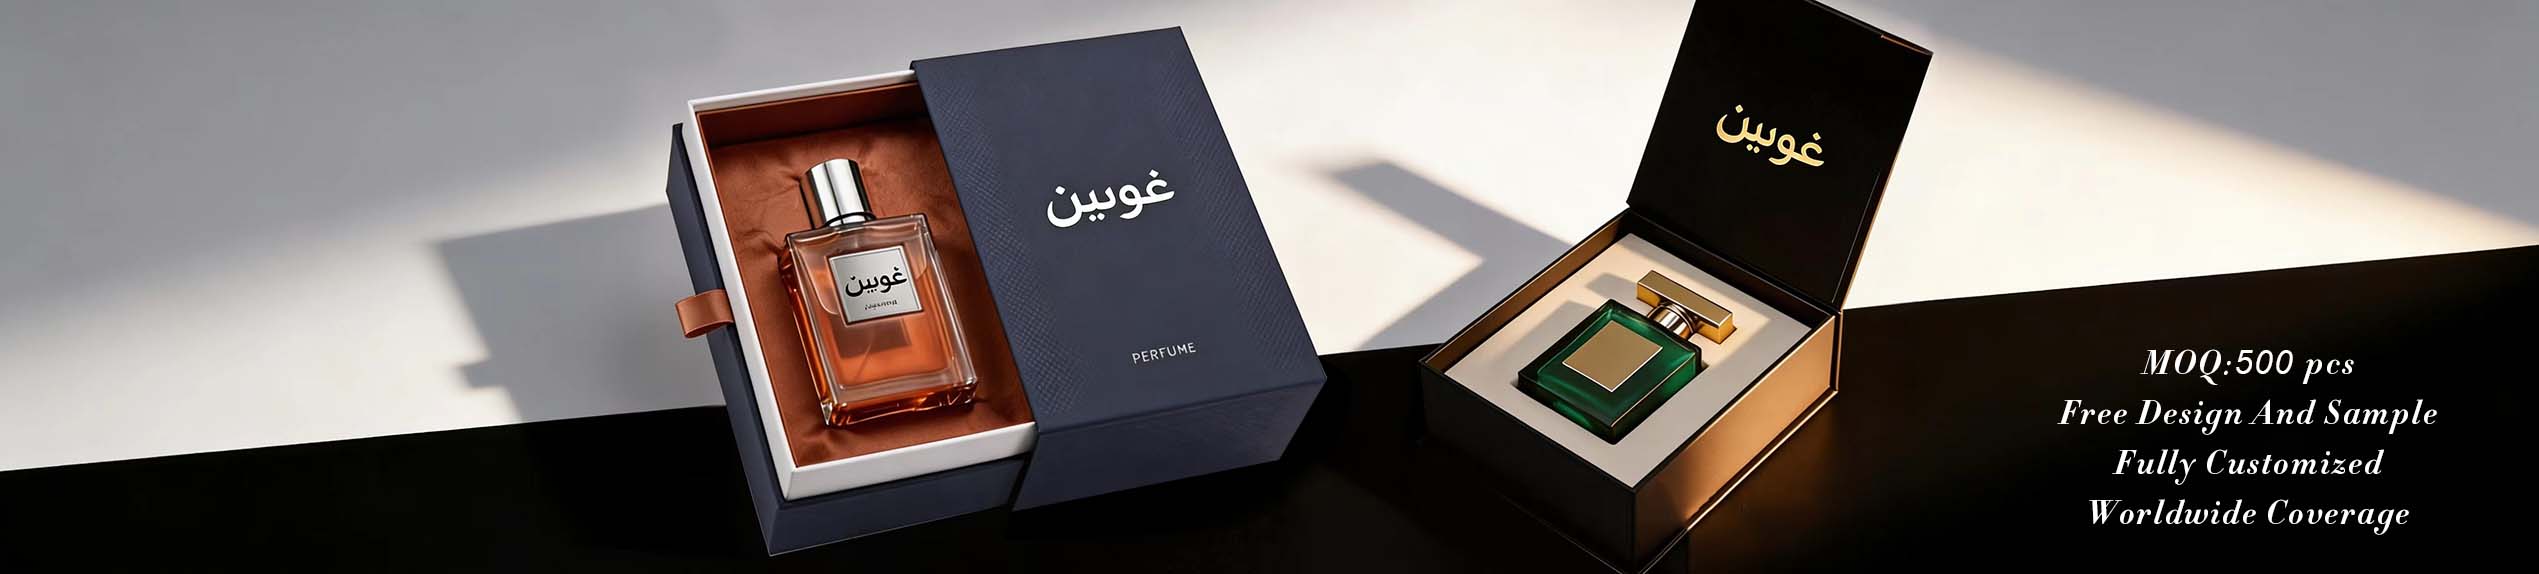
Perfume Packaging Sample Approval Guide: Workflow, Inspection, and Sign-Off
Approving a perfume box sample is where most launch delays are won or lost. This guide lays out the four sample stages, the exact checks to run on a physical sample, the tolerances to write into a sign-off sheet, and how to lock production against a golden standard.
What this guide covers
A typical perfume box programme runs in four sample stages: a white dummy (blank board to check size and fit), a digital proof (print and colour on the actual wrap), a pre-production sample (fully finished with magnet and insert), and a golden sample that is sealed as the production standard. Budget 7 to 14 days per round and 50 to 200 USD in sampling fees before tooling.
Brand, supplier QC, and often the filler line should all approve. The brand owns colour and structure; the filler confirms the bottle loads and unloads at line speed. Agree the approver list before the first dummy to avoid a late rejection that resets the clock.
Table 1 — Sample stages, lead time, and the decisive check at each.
| Stage | Purpose | Typical lead | Key check |
|---|---|---|---|
| White dummy | Size and fit | 3–5 days | Bottle clearance 3–5 mm |
| Digital proof | Print/colour | 3–5 days | Pantone delta-E <3 |
| Pre-production | Full finish | 5–7 days | Foil ±0.2 mm, magnet 3 N |
| Golden sample | Production seal | 2–3 days | Archive as standard |
Measure the assembled box against the dieline with callipers: finished size tolerance is ±0.5 mm for a standard box and ±1.0 mm for a large one. Drop the bottle in and confirm 3–5 mm clearance on each side with no rattle. On a book-style, close the lid and verify the magnet pull with a 3 N gauge.
Under 5000 K daylight, compare the wrap to the Pantone reference; accept a delta-E below 2.5 to 3. Run a fingernail and tape-pull test on hot foil applied at 110–140 °C to confirm adhesion, and check the V-groove spine for cracking where foil crosses the fold.
Document the golden sample with a signed acceptance sheet listing dimensions (±0.5 mm), foil registration (±0.2 mm), magnet hold (≥3 N), colour (delta-E <3), and AQL level for the run. Reference ISO 2859-1 with an AQL of 2.5 for major visual defects so production QC has a written bar.
Freeze the standard
Once the golden sample is approved, photograph it from six angles and archive the physical box. Production that drifts beyond ±0.5 mm or loses foil registration is then a documented reject, not a opinion dispute.
From the factory floor
Keep sample room at 23 °C and 50% RH per ISO 187 for stable dimension checks.
Use a 90° pull gauge for magnet hold; record in N, not 'feels OK'.
Release production only after the golden sample is signed and the AQL plan is agreed. First-piece inspection should compare the first 10 units to the golden sample before the line continues; full-run QC then samples per ISO 2859-1. Plan 15 to 25 production days after sign-off under FOB or DDP terms.
FAQ
How many sample rounds should I expect?
Plan for a white dummy, digital proof, pre-production, and golden sample — typically 7 to 14 days each, with 50–200 USD in sampling fees.
What tolerance is fair on box size?
±0.5 mm for a standard box, ±1.0 mm for a large one, measured with callipers against the dieline.
How do I stop colour disputes later?
Approve under 5000 K light to a Pantone reference at delta-E <3 and archive the golden sample with six photographs.
What AQL should the production run use?
ISO 2859-1 AQL 2.5 for major visual defects is a common, defensible bar for luxury fragrance cartons.
When is a magnet 'good enough'?
A closing hold of at least 3 N measured at 90° with a pull gauge; below that the lid can spring open in parcel transit.
Start your sample programme
GooinPack runs white dummy to golden sample in 2–3 weeks with a documented acceptance sheet. Send your dieline to begin.
Request a QuoteReferences


Blog Sitemap Xml Datenschutzrichtlinie
Copyright
© 2026 GuangZhou GooinPack Packaging Co., Ltd. Alle Rechte vorbehalten
.  NETZWERK UNTERSTÜTZT
Freundliche Links : Blogger
Eine Nachricht hinterlassen
Scannen zu WhatsApp :